Haskell Lemon Preserves Route 66, With Incentive
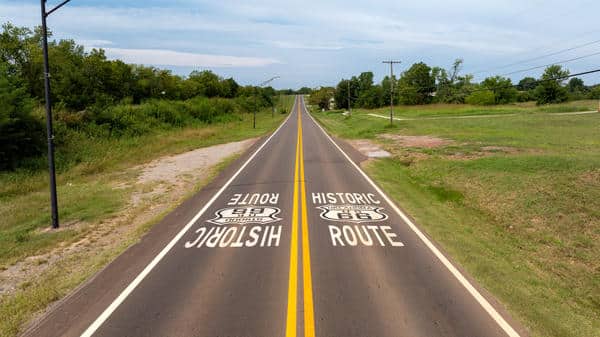
Route 66 Centennial pavement preservation celebration

As our nation celebrates its 250th birthday, its most famous highway celebrates its 100th. To recognize both, AsphaltPro Magazine is proud to highlight a 2025 pavement maintenance project on Route 66 near Chandler, Oklahoma, in which Haskell Lemon Group, headquartered in Oklahoma City, received a smoothness incentive for their good work. Here’s how they improved conditions on that stretch of the Mother Road.

Contractor’s New Museum Offers Glimpse of Route 66 History

Know Your History

Oklahoma Department of Transportation (ODOT) District 3 let the patching, leveling and surfacing project in spring 2025 to preserve 12 lane miles of a section of Route 66 outside Chandler. This involved milling part of the project, placing a ¾-inch leveling course and 1 ¼-inch surface course over all of it, and installing guard rail. None of this work was foreign to Haskell Lemon crews, which have performed maintenance and preservation along this historic roadway for decades.

Jay Lemon, president of the company and this year’s chair of the National Asphalt Pavement Association (NAPA), shared that they’ve been proud to work on sections of Route 66 within the state for as long as he can remember. In 2015, for example, they handled a project on the business road near Hydro and Weatherford.

A significant project he’s proud of took place in 2001 near Geary. For that one, the crews did more than repair the original concrete highway; they contributed to the nation’s history about this road.

Foamed Asphalt Preserves Route 66 in Missouri

“We removed six concrete slabs to be installed in the Smithsonian,” Lemon said. “We had to be gingerly with the process.” He explained that the team cut and removed the slabs, lifting them onto flatbeds for transport to Washington, D.C., where they are on display today.

For the Main Street of America, crews go where the road takes them. In 2022, Haskell Lemon performed a mill and overlay in the middle of a town. In 2020 and again in 2023, they worked on a section designated 66 north of Oklahoma City. It’s a proud moment to win a bid on the famous route.

Lemon explained that maintenance of Oklahoma’s stretch of Route 66 in the past typically consisted of bringing the highway up to new traffic conditions. “It was a 20-foot-wide, original concrete-paved road, and some sections are still that. But that’s way too narrow for today’s traffic. The majority is widened and replaced, so it’s a more durable product. Maintenance and widenings add 3 to 5 feet to either side and overlay it with asphalt.”

Celebrate our Shared History: https://theasphaltpro.com/route-66-road-construction/

Many of the preservation projects have seen the original 20-foot-wide, concrete-paved road repaired, widened 3 to 5 feet to either side, and overlaid with asphalt. Photo courtesy of Haskell Lemon

Maintain Your History

And that’s the structure his team worked on in 2025; a 24-foot-wide asphalt surface.

“In addition to the pavement patching and overlays, we installed widenings for approximately 40 locations to add guard railing, as a safety improvement,” Lemon shared.

In all, they placed about 19,700 tons of ODOT Type S-5 mix, which requires a PG64-22 binder. They included reclaimed asphalt pavement (RAP) for the ¾-inch leveling course. They produced this in their stationary CMI drum mix plant, averaging production temperatures of 320°F, located about 40 miles from the project.

“We call it our East Plant,” Lemon shared. It’s rated for 300 tons per hour, and for this project, “We averaged 150 tph.”

For paving, the crew used a CAT 1055F machine. “We utilize a CAT conventional paver with an Integral Spray Paver system added to it,” Lemon said. “The spray paver has been used on other US-66 projects, but this one was conventional paving with tack coat applied by distributor truck. We were able to maximize the smoothness incentive on this contract thanks in part to the grade/slope automation.”

Delta Brings Larry H. Lemon Award to Missouri

“We didn’t consistently utilize thermal mapping on this project, but did use a transfer vehicle for best quality and consistency throughout the whole job. We were seeing 290-310 degrees F behind the screed.” He reported the mix behaved normally at those temperatures for them.

To get compaction and build the joint, they used industry best practices.

“We paved two each, 12-foot-wide lanes. We would match centerline joints within one to two days to ensure that we could provide the best joint possible, before degradation could potentially occur. We utilized a combination of CAT double drum and Dynapac double drum rollers in our rolling train.”

The rolling team was exemplary in their work.

“No intelligent compaction technology was used. We utilized portable density measuring devices to monitor and ensure quality compaction. Our gauges were showing acceptable, and no cores were required as the lifts were too thin to utilize that practice.”

Ten DOTs Garner Perpetual Pavement Awards with Asphalt

Instead of cores, the gauges used by Haskell Lemon and ODOT proved the team’s success. Lemon shared that they used an “ODOT-approved rolling pattern with verification occurring every day. This was successful for both teams.”

“They completed all of this work with zero accidents, internally or to any of the motoring public,” Lemon said proudly. “This is huge considering the tight working conditions and the rural nature of the project,” which included flagging operations on the two-lane interstate. “We were pleased with how the project was planned and performed.”

Considering the high-profile nature of the historic roadway, having a successful project executed with no accidents is its own reward. Add to that receiving an incentive for its smoothness, and the Haskell Lemon team has even more to be proud of when pointing to their participation in the Mother Road’s centennial celebrations this year.


Share Your History

Has one of your asphalt crews worked on Route 66? Share that with the wider asphalt audience!

Reach out to Sandy Lender at AsphaltPro Magazine so we can write about your project and what that project meant to you. Email sandy@theasphaltpro.com

And if you’re reading this while at CONEXPO-CON/AGG, stop by booth GL30901 to chat in person.

Echelon Paving Powers APEX Motor Club Expansion

Sunland Adds to APEX Motor Club with Quality Echelon Asphalt Paving

The high-speed world of motorsports demands world class precision, performance and durability. At Sunland Asphalt & Construction, LLC, Phoenix, we embraced these principles when we took on the development of the second circuit at the APEX Motor Club track in Maricopa. Spanning from August 2024 to February 2025, this project represents an incredible milestone in Arizona’s racing landscape.

The transformation of undeveloped farmland into a high-performance racetrack required extensive engineering and meticulous attention to detail in planning. Phase two took place from August 2024 to February 2025.

Transforming Dream Into Reality

The transformation of undeveloped farmland into a high-performance racetrack required extensive engineering and meticulous attention to detail in our planning. Grading was a critical component, with 138,960 cubic yards of material cut and 121,163 cubic yards of fill placed to shape the building pads, retention basins, multiple track sections, runoff areas and paddocks.

Huron Capital’s Platform Sunland Asphalt Acquires Georgia Paving

For the track’s foundation, an 8-inch layer of Aggregate Base Course (ABC) was placed and finish graded before receiving a 2.5-inch application of ½-inch asphalt—meaning ½-inch nominal maximum aggregate size (NMAS). The track itself was surfaced with 1.5 inches of a 3/8-inch Special Mix for the wearing course, ensuring superior grip and durability. Our use of echelon paving—simultaneously running three pavers—was key to achieving a seamless, high-quality racing surface.

A binder course of 2.5 inches of ½-inch material required 100% of the aggregate should pass through the ¾-inch sieve. The surface course of 1.5 inches of 3/8-inch Special Mix required 100% should pass through the ½-inch sieve.

“During echelon paving, we utilized three material transfer vehicles (MTVs): two Weilers and one Roadtec Shuttle Buggy,” said Greg Hughes, our project manager – Public Works. “Paving operations were carried out using three Vogele Super 2000-3i pavers. Paving this way almost eliminates any joint and acts as one continuous mat. The slope of the track was minimal, so additional support equipment was not required during rolling operations.”

“At the transverse joints, we used a 12-foot straightedge to check for flatness and made necessary adjustments to maintain levelness. Along the outer edge tie-ins, we aligned the screed to match the elevation of the existing asphalt for a seamless transition.”—Greg Hughes

Race to Resurface F1 Track

A Track Built for Enthusiasts

APEX Motor Club, now owned by RJT Capital, is more than just a racetrack; it’s a haven for speed enthusiasts. Strategically located to serve Phoenix, Tucson, and even cities like Los Angeles and Albuquerque, this circuit caters to drivers who demand the best. Every detail, from the material selection to the construction techniques, was geared toward delivering a world-class racing experience.

The two sections of the track Sunland has now completed can be run independently or combined into a single 4.7-mile configuration for racing.

The track’s continuity with Phase 1, which we paved in 2018, was another highlight of this project. Ensuring seamless integration required exceptional precision in tie-in joints and elevations. The result is Arizona’s longest motorsports track—a continuous circuit designed to push limits and set new standards in high-performance driving.

“The original track measured 2.27 miles, while Phase 2 added an additional 2.43 miles,” Hughes shared. “These two sections can be run independently or combined into a single 4.7-mile configuration.”

Traffic Control Success on Mesa’s US-60 Corridor

Precision Paving at it’s Best 

One of the most demanding aspects of this project was achieving the track’s stringent surface tolerance. That quality started at the base.

“To ensure grade tolerance, our blade utilized GPS technology to follow the project-specific model accurately,” Hughes explained. “At the transverse joints, we used a 12-foot straightedge to check for flatness and made necessary adjustments to maintain levelness. Along the outer edge tie-ins, we aligned the screed to match the elevation of the existing asphalt for a seamless transition.”

Echelon paving, which was crucial to ensuring consistent quality across the track’s 42- to 50-foot width, can have many complex logistical challenges in coordinating multiple paving machines and maintaining uniform asphalt application.

Project Foreman Isidro Lopez was one of the key figures in bringing the project to life. He stated, “Spending time with family is my favorite way to unwind,” but on the job, he played a vital role in delivering the precision the track required.

“Since GPS technology was used to establish the desired grade during preparation, we paved using a 2D control system,” Hughes explained. “Each paver was equipped with 30-foot paving skis, which helped maintain consistent depth and alignment. The skis function as a leveling system by averaging the surface over their full length, effectively smoothing out minor grade variations. Additionally, the second lift served as a corrective layer, addressing any imperfections remaining in the base course.”

Additionally, Sunland installed 4,850 feet of concrete curbing designed specifically for APEX, improving both functionality and aesthetics. Our team also constructed a 100-foot by 85-foot box culvert and 1,020 feet of cut-off walls to manage water flow and enhance track stability, ensuring optimal performance under diverse conditions.

A binder course of 2.5 inches of ½-inch material required 100% of the aggregate should pass through the ¾-inch sieve. The surface course of 1.5 inches of 3/8-inch Special Mix required 100% should pass through the ½-inch sieve.

Key Partners

This project was a collaborative effort, made possible by our trusted subcontractors:

  • Solterra Materials supplied the high-performance, polymer-modified asphalt, ensuring superior grip, durability, and smoothness. Led by Michael Thompson, Solterra’s expertise in asphalt production and logistics was instrumental in maintaining project timelines and quality.
  • Vital Contracting, under the leadership of Stephen Boyd, executed all earthwork operations, delivering near-perfect tolerances essential for racetrack construction.
  • CMT Technical Services, headed by DJ Peters, ensured compliance with rigorous material testing standards, performing geotechnical evaluations, density testing, and asphalt mix verification.

A truck has completed loadout at the Solterra Materials plant and is ready to take a load of mix to the APEX Motor Club track project.

Spotlight on Isidro Lopez

One of the key figures in bringing this project to life was Isidro Lopez, project foreman at Sunland Asphalt. With years of experience in the industry, Lopez played a vital role in delivering the precision required for a world-class track. He stated his favorite aspect of this job was, “Seeing the owner’s excitement when we finished—it was like kids opening Christmas gifts.”

Project Foreman Isidro Lopez was one of the key figures in bringing the project to life. He stated, “Spending time with family is my favorite way to unwind,” but on the job, he played a vital role in delivering the precision the track required.

The most memorable day for Lopez was, “Reaching the end of the track on that final day of paving—everyone was thrilled to achieve the end goal.”

“Seeing the owner’s excitement when we finished—it was like kids opening Christmas gifts.”—Isidro Lopez

A Legacy of Excellence 

On this issue’s front cover, from left to right, Will Morrison is the asphalt plant operator for the Coolidge site and Matt King is an asphalt plant foreman for Solterra Materials, the company that supplied the high-performance, polymer-modified asphalt for Sunland’s APEX project.

Sunland Asphalt & Construction’s commitment to precision and innovation continues to drive our success. The completion of APEX Motor Club Phase 2 marks yet another milestone in our legacy of delivering top-tier asphalt solutions. From engineering complexities to flawless execution, this project exemplifies our expertise in high-performance paving—ensuring that APEX remains the premier destination for automotive enthusiasts across the Southwest.

For those who live life in the fast lane, APEX Motor Club is ready. And Sunland Asphalt & Construction is proud to have paved the way.


Immanuel Martinez brings 20+ years of experience managing complex construction projects, pioneering 3D paving innovations, and leading high-performing teams across public and private sectors. To learn more about Sunland, visit sunlandasphalt.com and check out past articles on TheAsphaltPro.com.

Race to Resurface F1 Track

Sunland Asphalt performs mill and fill on Miami Formula 1 track with echelon paving ahead of successful Grand Prix

In the Formula 1 world, millimeters matter in both racing and paving. Management at Sunland Asphalt & Construction, Littleton, Colorado, knew they would need their A team on hand to handle the 2023 resurfacing project at the Miami International Autodrome, home of the Formula 1 Miami Grand Prix. They mobilized 75 internal employees, 15 technical specialists and 40 pieces of heavy equipment from around the country on 35 separate transport loads.

The project’s scope consisted of milling 2 inches of the existing track and repaving it with a highly specialized asphalt mix designed to Formula 1 standards. Crews were to repave the track at 2 inches thick for a total of 9,500 tons over an eight-day period.

Construction scheduling for the 3.36-mile anticlockwise circuit, which winds around the Hard Rock Stadium in Miami Gardens, had to be choreographed around the stadium’s other events, including the end of the National Football League season, a jazz music festival and the Miami Open tennis tournament. The International Automobile Federation also required Sunland to have the mix put down 60 days before its big event for the material to properly cure.

Needless to say, it took a lot of coordination for Sunland to make this happen and the Wirtgen Group was just one of the many partners in place to help.

Sunland crews used three pavers working in echelon to prevent cold joints along the 50-foot-wide track, paving at a very efficient pace of only 6 fpm.

Step 1. Mill. The crew from Sunland Asphalt & Construction, Littleton, Colorado, used three milling machines to precisely remove 2 inches from the existing track.

The Need for Speed—and Grip

In 2022, Miami held its first Grand Prix event on the track. When drivers expressed concerns with the grip on the pavement, track owners decided to lay fresh asphalt ahead of the 2023 race. The track management hired Tilke Engineers & Architects, headquartered in Aachen, Germany, to oversee track resurfacing, which they said would ultimately improve the “spectacle” of the 2023 race.

Sunland was hired to complete the mill-and-resurface of the track and began work to remove the existing surface in the early spring of 2023.

Sunland Asphalt trucked all their equipment in to ensure crews were familiar and comfortable with their equipment and processes. They used three pavers working in echelon to prevent cold joints along the 50-foot-wide track. The pavers were also moving at a very efficient pace of only 6 fpm to ensure paving smoothness.

The mix design for the track included 60% US-mined granite from Georgia with the remainder of the aggregates being locally sourced lime rock from Southern Florida. These aggregates ensured the grip needed on the course.

Step 2. Fill. Three pavers worked in echelon at a steady pace of 6 feet per minute to ensure no cold joints interrupted a smooth mat. Here you can see a Weiler material transfer vehicle feeding the hopper insert of one of two Vogele Super 2000-3i pavers to assist in smooth, constant material control.

Technology Meets Tight Tolerances

In addition to the three Wirtgen mills, Sunland used three HAMM HD+ 80i rollers and two VOGELE Super 2000-3i asphalt pavers. The Wirtgen Group technology on these machines is “plug and play,” which allowed the team at Sunland to get up and running with these machines easily.

“The plug and play feature on all these machines has been a huge advantage to us as a Topcon provider, making the installs quick and easy,” Tony Carden, intelligent paving product manager at RDO Equipment said. “We’re also able to provide serviceability for them both on the dealer side and from the manufacturer side. It’s a win-win.”

The project’s scope consisted of milling 2 inches of the existing track, then repaving 2 inches thick with a highly specialized asphalt mix designed to Formula 1 standards, for a total of 9,500 tons over an eight-day period.

Thermal Imaging

The pavers on the job were equipped with a temperature monitoring system. Thermal cameras were mounted to the pavers and used to find any temperature differences that could indicate potential segregation in the mat as it was being laid.

“The thermal profiling that we’re using on the pavers gives a rundown of where the pavers were, where they’re going, at what speed they are running and at what temperature,” Greg Hughes, project engineer at Sunland said. “If one isn’t getting to a high enough temperature, we can go back and look at it and see what happened and fix it and that’s a great tool for us.”

To address racecar drivers’ concerns about pavement grip, the Miami International Autodrome’s Formula 1 Miami Grand Prix track was milled and resurfaced ahead of the 2023 big event. All photos courtesy of C2C Visuals

To address racecar drivers’ concerns about pavement grip, the Miami International Autodrome’s Formula 1 Miami Grand Prix track was milled and resurfaced ahead of the 2023 big event. All photos courtesy of C2C Visuals

Intelligent Compaction

“The intelligent compaction on all the rollers shows us our roller patterns throughout the day,” Hughes said. “It provides us real-time documentation of the areas we are hitting and if we’re hitting any areas more than we should. We’re also able to know if we should be vibrating more or less as well.”

With the HAMM Intelligent Compaction system, users can set a designated number of passes ahead of paving. The system shows the operator, on the in-cab display, how many passes have been completed.

Sunland management says they also use the intelligent compaction system as a training tool. “We sit with our roller operators, and we can show them where we might be able to improve on future jobs.”—Greg Hughes

Step 3. Compact. The compaction team set a rolling pattern behind the pavers to achieve optimum densities and a smooth driving surface incorporating three HAMM HD+ 80i rollers.

Sunland management says they also use the intelligent compaction system as a training tool.

“We use it in the office to see where we could be more effective,” Hughes said. “We sit with our roller operators, and we can show them where we might be able to improve on future jobs.”

The crews finished paving the 19 turns of the course on the Autodrome’s schedule, and the 2023 Miami Grand Prix was a success thanks to the hard work and dedication of the people behind the machines.

NB West Wins with Smooth Asphalt Results, Again

Balancing GTR, RAP, WMA over failing concrete proves successful for Missouri taxpayers

Early June 2023, the team at NB West Contracting, headquartered in Pacific, Missouri, began work on a complex overlay. The main goal was to cover up a 15.3-lane-mile, potholed, concrete section of Route 63 in Maries County and make it a smooth, safe driving surface for the taxpayers. The Missouri Department of Transportation (MoDOT), Ingevity, National Center for Asphalt Technology (NCAT) and NB West partnered to exceed that goal.

Steve Jackson, the vice president of asphalt plant operations and sustainability for NB West spoke of combining ground tire rubber (GTR) and 20% recycled asphalt pavement (RAP) as one aspect of the warm-mix asphalt (WMA) project.

Jackson took infrared images of the project to double-check consistency of mat temperatures and confirmed that consistency coming from the plant to the jobsite.

“It was a balanced mix design, performance spec, SP095C (9.5-millimeter,) Superpave with ground tire rubber and RAP, warm mix, placed through a spray paver, and bonding to a concrete pavement,” he said. He listed off all those moving parts of the project like it was business-as-usual for the production and paving personnel. For a team that’s been on the scene since 1956, it almost is a walk in the park, yet they pulled out the quality control/quality assurance (QC/QA) and safety best practices to make sure everything flowed smoothly for an award-worthy project. In the end, they garnered the Missouri Asphalt Pavement Association (MAPA) 2023 award for a primary route under 50,000 tons. Here’s how they accomplished it.

Familiar Parameters

In 2012, NB West had successfully performed a project bonding an asphalt layer to concrete with the company’s Roadtec spray paver, and saw an opportunity to apply that technology again. Jackson explained the DOT originally was letting the project with the 19.0 mm mix and a 12.5 mm mix for the surface layer, but his team wasn’t excited about that because both layers would have been placed at less than four times the nominal maximum aggregate size.

“The thickness of the layer didn’t allow for the 12.5 mm to work smoothly,” he said. “In 2012, we’d done something similar bonding concrete with the spray paver, so after we were awarded the [Maries County] job, we did a value engineering proposal to bond to the concrete. We suggested two lifts of 9.5 mm Superpave with an overall reduction of 1 inch in the overlay. We’ve been trying to get back to realistic lift thicknesses that can get good compaction and DOT agreed with that.

The Relationship Between EPDs, BMD, RAP & Plastic

“We also proposed using ground tire rubber to delay the cracking coming back through the mix. The other reason for the GTR is we were doing our performance tests, and when we’re using the GTR in those mixes, our IDEAL-CT numbers have just been off the charts. Our performance tests are the IDEAL-CT and the IDEAL-RT.”

Good Numbers: For the Maries County project, the team saw an average CT-Index of 168, an average RT-Index of 77 and Hamburg rutting result of 7.0 mm.

The unconfined joints were on the outer edge of a concrete roadway that had a rock shoulder. The NB West crew paved the mainline and used a non-Superpave asphalt layer over the rock to cover up the shoulder.

Making Mix

Jackson credits the elasticity of the GTR for aiding in pavement performance. “We’re putting the ingredients back in that gives it a little flexibility.”

To add the GTR, NB West uses the dry process, adding Elastiko® engineered crumb rubber asphalt (ECR) manufactured by Envirotx and supplied by Asphalt Plus. N.B. West’s Joe Schroer, P.E., materials and support engineer, explained the dry process is considered mixture modification. Performance testing measures the interaction of GTR, aggregates and binder as a system, and allows a more innovative approach to designing asphalt mixtures, he shared. Additional enhancements to mixture performance can be made by adjusting the grade of the binder.

A groundman brings the 2,000-pound tote of Elastiko material to the feed bin of a modified Hi-Tech Fiber machine with a forklift. From the bin, the machine feeds the material to a 6-inch-diameter flexible hose and to the portable Astec Double Barrel.

Balance Your Mix Design for Asphalt

“We blow it right into the drum,” Jackson explained. “The control unit’s inside the control house and it’s tied into the tons per hour you’re producing.” In this manner, the plant controls the addition of the GTR product as it would cellulose fibers being fed in.

This project ended up with a variety of additives in the production process, but Jackson said it was business as usual for the team. “We had the normal challenges. This still had our normal Superpave testing in it; we were still running volumetric testing and adding in the performance testing. So, it was a lot of testing.”

Jackson shared a testing tip for working with GTR. “When you’re making pucks up, if you put a weight on your mold top (with the GTR in there), it keeps the GTR from rebounding while cooling. If you don’t do that, you get some kinda strange results.”

The unconfined joints were on the outer edge of a concrete roadway that had a rock shoulder. The NB West crew paved the mainline and used a non-Superpave asphalt layer over the rock to cover up the shoulder.

Smooth Quality

In the field, the crew worked with temperatures below 300 degrees F. Even with the Evotherm WMA additive in play, they elected to have temperatures closer to HMA to accommodate the Elastiko. “The manufacturer told us not to go below 280 with the GTR,” Jackson said. “We went down to 270 and didn’t have any problems.” A longer haul—approximately 40 minutes from the plant—for this project allowed a longer dwell time for interaction of the GTR with the binder at the reduced temperature, according to Schroer.

Jackson took infrared images of the project to double-check consistency of mat temperatures and confirmed that consistency coming from the plant to the jobsite. “I took my FLIR camera out there…the good thing is I think the ground tire rubber holds the heat in the mixes. It was about 40 minutes to the job, and we were on a two-lane road where we had to flag the traffic, so it was challenging getting the trucks in and out. But we didn’t lose a lot of heat in the mixes.”

One of the best practices Jackson recommended was staying on top of the rolling pattern. “We were keeping our rollers right up on the screed. Because we were already dropping our temps below 300.”

The mix design used all the moving parts. “We used 20% RAP in this mix and 10% by weight of AC was the asphalt plus Elastiko product. The idea was that we had our baseline AC, which was a 64-22 and 10% of the Elastiko was in there to bump it up to a 76-22. It was the same mix on both lifts.”

Is Your Lab Ready for Balanced Mix Design?

The Missouri DOT allows whatever percentage of RAP the contractor wishes to use and still meet performance specs. “Technically, there’s no limit,” Jackson said. “Our problem is availability. We can’t run maximum RAP in our mixes because we don’t have it. There was nothing to mill on this project, so we had to bring RAP from other locations to put in this mix.”

For the NB West team, that’s just one more solvable problem. Jackson spoke of the “can do” willingness to put a puzzle together when it comes to the crew, starting with Plant Operator Clay Pitts.

“Number One is just the general attitude of not saying ‘we can’t do that.’ Yeah, we’ll try that. That’s huge. Clay’s great about that. Always willing to try something new and make it work.

“Dustin Hollis was the foreman and Juan Marquez was the general superintendent; they manage several jobs at a time.”

Jackson also described the effort the quality control/quality assurance (QC/QA) team had to put forth, given the changes to the contract after it was bid.

“Our quality control dept came up with these mixes and tried new things and really kind of pushed the envelope. The performance testing, the way we did this, that wasn’t set up in the contract, so we still had to do all the volumetrics testing and add the performance on top in a BMD situation. We’ve never run this mix so we were going live on the road with what looked in the lab like it would run well and do its performance testing. We had to go behind the spray paver and dig a sample behind the screed in a mat that has a polymer in it. It was a monumental challenge for our QC team.

“We have our plant people and our QC people coming up with this crazy stuff and then we go execute it and we still have to make money at it. I think we did a slight tweak to the mix after the first day or two to take advantage of the performance test because we could reduce our air voids using the performance test.”

The final result gave an average international roughness index (IRI) of 32.

“On concrete pavement that they didn’t have enough pavement repairs for, to come out like that, I think it was great,” Jackson said.

Not only did the project win a MAPA award, the traveling public noticed the good work. Jackson has received unsolicited comments about the work. “I’ve had somebody call and say, ‘that rides real good.’ People see that [kind of result] and they’re more likely to support the gas tax.”


Balancing Mix for Optimum Density

One of the reasons NB West uses a warm-mix additive in every mix they can is to get the compaction aid assistance.

“We run Evotherm in every mix that we have to get density on,” Jackson said. “We don’t run it on Novachip, but every other mix, we’re putting it in there.”

One of the factors that changes when developing a balanced mix design (BMD) and doing your performance testing is the number of gyrations.

“You’re dropping your gyrations,” Jackson said. “You’re making a mix that’s got more AC in it. So, you can take advantage of some of those mixes then of making them more compactible in the lab so when you go to the field, it’s easier to get compaction.”

Take a typical interstate mix as an example.

“We started off at 125 gyrations on interstate mixes. When you’re trying to compact that, you’re breaking rock trying to get density. Then we backed off to 100 gyrations, then to 80. I think we’re at 60 with BMD.

“To keep your voids in mineral aggregate (VMA), you end up putting some more AC in it. So, you have a mix that will compact, and it’s got binder to hold it together. Now instead of breaking rock to get to 92%, you’re rolling this and getting 96%. That’s what FHWA wanted: higher density. We get higher density by going to balanced mix design.”


Learn More

Step 1: The forklift brings the tote of ground tire rubber product to the bin.


Step 2: The GTR product is fed through the 6-inch-diameter, flexible hose.


Step 3: The plant’s controls meter the product just as it would any cellulose fiber being fed to the Astec Double Barrel drum.

Cobleskill Rehabs Two Stretches of I-88

Established in 1954 with the purchase of a limestone quarry in Cobleskill, New York, Cobleskill Stone Products Inc. has grown into an aggregate producer, material supplier and construction services provider for upstate New York. When it comes to asphalt paving jobs, a large portion of the company’s business revolves around overlays for states, counties and municipalities. Recently, the firm used a Dynapac MF2500CS mobile feeder to help pave two rehabilitated stretches of I-88—one near Schenevus, and the other near Central Bridge.

“Continuous paving also eliminated bumps in the mat from the machine stopping and letting the screed settle, which resulted in a more consistent and higher quality finished product.”—Sam Galasso

Minnesota Contractor Improves Efficiencies and Productivity with Asphalt Milling Tool

Multiple Lifts, Smooth Results

“The Central Bridge project included three lifts of blacktop to put down,” explained Michael Moore, vice president of Cobleskill Stone Products. Those were a base, binder and top course.

“The job specs only required using a material transfer vehicle (MTV) for the binder and top course, but we chose to use one for all three courses,” added Dan Mark, the project superintendent on the Central Bridge project.

Mark explained that using an MTV allowed the crew to eliminate truck transitions, lay more tons at a consistent speed, and provide “better rideability.”

With a Dynapac MF2500CS mobile feeder, an operator transfers asphalt from a truck to a paver at Cobleskill Stone Products’ I-88 rehabilitation job in upstate New York.

Job specifications for the MTV included a 30-tonnage capacity between the MTV and the hopper.

“We looked at multiple brands before choosing the Dynapac MF2500,” Moore said. “Using a tracked machine opposed to a wheeled machine had specific appeal because we were working with crack and seat material. Once we established the carrying capacity met the job specs, we looked at the remix capabilities built into the machine and the oscillating conveyor, and it was clear the machine fit the bill for how we wanted to approach the project.”

How to Patch with Infrared Tech

The Dynapac MF2500CS mobile feeder has a maximum operating speed of 82 feet per minute and a feed capacity of 2,000 tons per hour, when using an optional swing conveyor, or a feed capacity of 4,000 tons per hour with a standard conveyor.

At the I-88 Schenevus project, Cobleskill Stone Products’ operators typically laid 17 feet of asphalt per minute, totaling upwards of 3,000 tons of material per day, which allowed them to complete echelon paving with two pavers running side-by-side for a portion of the project.

From left to right, Cobleskill Stone Products Inc.’s Sam Galasso, Michael Moore and Dan Mark; Tom Kiselica, paver and feeder marketing developer at Dynapac; Mike Moore Jr., quality control manager at Cobleskill Stone Products; and Steve Kenney, sales representative at Anderson Equipment Company, work together.

“One of the days, we were able to lay almost 3,400 tons of material,” noted Sam Galasso, supervisor. “The MF2500 helped tremendously with production and eliminated the cold joint in the center of the mat. Continuous paving also eliminated bumps in the mat from the machine stopping and letting the screed settle, which resulted in a more consistent and higher quality finished product.”

“Machine uptime for the I-88 project was 100%,” Moore said. “The user-friendly interface made it easy to operate and allowed our operator to train other employees to run the machine.”

Dealer Support

When looking for the right machine for the I-88 project, Cobleskill Stone Products turned to Steve Kenney, a sales representative at Anderson Equipment Company, and Tom Kiselica, the paver and feeder marketing developer at Dynapac.

“The machine was fit for this job site,” Kenney said. “The controls are directly in front of the operator, who can operate the machine from either side of the cab.”

Cobleskill Stone Products also relies on Anderson Equipment Company and Dynapac for support.

“Both Tom and Steve have been excellent,” Moore said. “They checked in on the job’s progress and machine’s performance multiple times. We’ve worked with them before and know that they go above and beyond to make sure our Dynapac equipment is running.”

Vögele’s Passive Remixing Insert with an Active Remixing Module

Hopper inserts can be helpful to increase the volume of asphalt material you can carry, but they can also assist in avoiding segregation of your asphalt mix. That’s the idea behind the passive remixing insert with an active remixing module from the team at Vögele, a division of Wirtgen America, Antioch, Tennessee. Here’s how it works.

With the use of a material transfer vehicle, asphalt mix is delivered to the hopper insert. It can be loaded between two baffles located within the insert, which limit gradation segregation. The maximum capacity of the insert, when filled only between the baffles, is 17 tons. However, operators can also overflow the baffles, as the company literature states, to make use of the full 23-ton hopper.

“Anytime you create a pile, you allow larger stones to roll on the sloping face until they stop, and they stop when they hit the wall of the insert,” said Laikram “Nars” Narsingh, manager, commercial support and development for Vögele. “The baffles allow material to funnel straight into the flight chain to prevent larger stones from rolling to the sides.”

Between the baffles, there is a grate system to break up cold crusts as they enter the insert. This combats not only gradation segregation, but also thermal segregation by allowing smaller clumps to absorb heat from the hotter surrounding mix.

The grate system is located more than a foot beneath the top of the baffles to allow operators to pile asphalt on top of the grate so that the increased weight forces the material through the parallel grate bars, which are spaced between 3 and 8 inches apart.

After passing through the grate, the mix travels down to the base of the hopper insert. Since the front of the insert is wider, material flows from the front of the insert to the back of the insert to minimize thermal segregation. This wider, overhanging front of the insert also expands its total capacity.

The material then passes through the trapezoid-shaped opening on the bottom of the insert, which also aims to reblend mix naturally as stones move along the sides of the insert, and is then discharged onto the conveyor of the asphalt paver.

For more information, contact Narsingh at (615) 501-0600.