INDOT Uses CCPR with AMICYCLE Emulsion Additive to Restore SR236
BY Olivia Kortepeter

Embracing greener roadway strategy: cold recycling mix design at work
Across the United States, road management agencies are moving beyond conventional repaving methods, embracing cold pavement recycling treatments to reduce environmental impact and stretch their budgets further on critical infrastructure.
Since 2018, the Indiana Department of Transportation (INDOT) has specified Cold Central Plant Recycling (CCPR) treatments on six state route rehabilitation contracts. Their treatment selection has been crucial to project success, through thoughtful consideration of options paired with an understanding of the in-situ pavement structure and the long-term needs of the network. In adopting CCPR as a rehabilitation technique, INDOT has gained a cost-effective, reliable and sustainable solution.

This diagram shows the profile of the State Route 236 project.
CCPR begins by milling reclaimed asphalt pavement (RAP) from a roadway and storing it at a nearby stockpile site. Often, with the majority of asphalt pavement removed, more invasive work can be done below the pavement whether utility excavation, subgrade treatment, or testing and inspection of underlying materials. Upon completion, a mobile mixing unit (pugmill) at the stockpile site blends the sized RAP with an asphalt emulsion, creating the CCPR mixture. The resulting mixture is then returned to the roadway as an intermediate pavement lift, reducing the demand for new materials.

The crew milled the existing asphalt 8 inches deep.
A Closer Look at the State Route 236 CCPR Project
One of INDOT’s earliest and largest CCPR projects took place on State Route 236. During the 2021 and 2022 construction seasons, contractors collaborated to transform 13.36 miles of a narrow road with yielding subgrade into a wider, stabilized pavement structure topped with a hot-mix asphalt (HMA) surface course.
To minimize disruption, the project was executed in phases to accommodate local traffic. Each segment followed a multi-step rehabilitation process lasting approximately two months:
- Sampling and Mix Design: Pavement engineers took samples of the roadway material. In a lab, they designed and tested the correct composition of materials to create the new paving mixtures.
- Milling Existing Asphalt: The asphalt was milled to a depth of 8 inches, and the RAP was transported to a central processing yard no more than 10 miles from the site, minimizing haul times and emissions.
- Full Depth Reclamation (FDR): A nominal 3 inches of corrective aggregate was added to the exposed road base, then pulverized to a depth of 10 inches and stabilized with Portland cement.
- Creating the CCPR Mixture: The RAP was crushed, screened and sized to the required specifications before being mixed with a specially formulated engineered asphalt emulsion in a specially designed mobile mixing plant.
- Paving and Layering: Trucks delivered the CCPR mixture back to the job site, where it was laid in two 3-inch lifts using standard paving equipment. A 2-inch HMA lift was applied as the surface course, followed by permanent pavement markings.
This process not only optimized material reuse but also demonstrated the adaptability of CCPR in combination with other treatment types to tackle a variety of roadway conditions in a manner reflective of reconstruction.
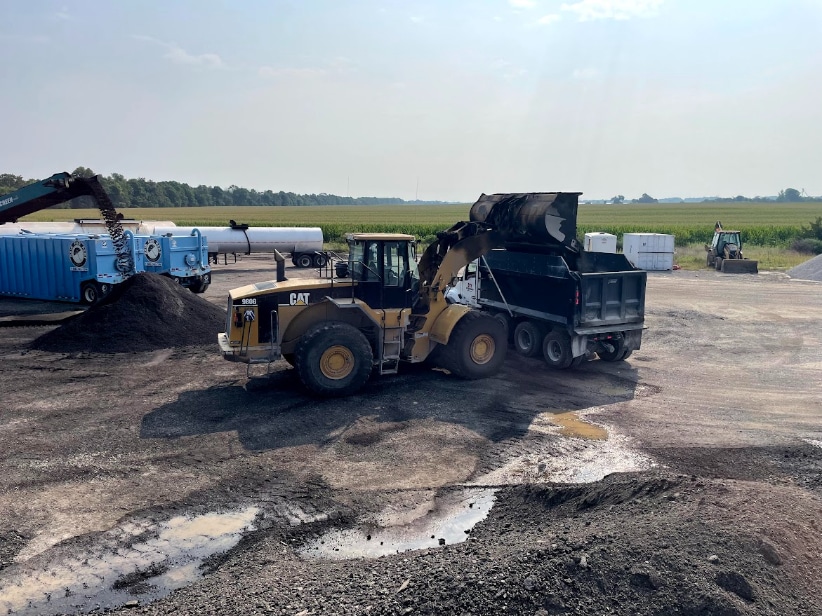
At the cold central plant recycling yard, the mix is blended in the pugmill and loaded into trucks for delivery to the job site.
Deep Dive into CCPR Mix Design and Adaptability
Asphalt Materials Inc. (AMI) developed this specially formulated emulsion, branded as AMICYCLE. The CCPR mixture was sampled in the field and then laboratory-designed by Heritage Research Group (HRG). Their mix design was specific to the materials present and the construction details specified in the project plans. Quality Control (QC) for the CCPR was also overseen by HRG, ensuring the mixture met the standards outlined by the specification.
Mix Design Process
In the lab, the RAP was crushed down and mixed with the engineered emulsion, which can be adjusted based on the expected temperatures and haul times, to produce 4-inch-diameter (100 mm) specimens for testing. The team created these specimens from both a medium and fine gradation, each mixed with three different levels of emulsion content. These six combinations underwent compression by a hydraulic press to test for stability and rutting resistance. Testing ensured the mix met durability standards before full-scale production.
With the optimal mixture selected, the HRG team worked closely with the pugmill operator to ensure the CCPR mix was precise, following the specifications outlined by INDOT for mix design and testing. HRG performed QC checks on the RAP gradation and mixture ratios throughout the process to ensure accuracy.
The mobile mixing plant (pugmill) used for the CCPR was custom-built by Pugmill Systems in Columbia, Tennessee. “AMI commissioned this unit to fit a specific combination of criteria not met by other machines on the market: tons per hour, ease of transportation and variable temperature handling,” said AMI’s Bruce Wehr. “[This] pugmill was designed to process a higher volume, up to 300 tons, of material per hour. Even with increased machine capacity and size, the unit was built with less weight so it could be hauled without permits, unlike many other pugmills. Finally, this machine had a wide operation range for liquid temperatures, handling materials ranging from CCPR at 100 degrees to Cold Patch at about 300 degrees. The Allen Bradley operating controls and mass flow meter allowed for this diversity of temperatures. With these capabilities, AMI’s custom mobile mixing plant was optimized for CCPR production.”
Once the CCPR mixture was placed, nuclear density gauge testing was performed to optimize the mixture’s compaction to ensure consistency and long-term performance. HRG monitored the curing of the CCPR lift, which can range in duration from 2 to 10 days, depending on environmental factors. INDOT specification requires the CCPR mat to reach a moisture content below 3.0% prior to HMA paving. The roadway was opened to local traffic immediately following the finish rolling operations.
Besides this meticulous testing and QC, continuity was another key to success. The same team that sampled the roadway’s millings also designed the mix and performed quality control throughout the entire process.

Here the team paves the first of two 3-inch lifts of cold central plant recycling (CCPR) mix made with AMICYCLE, a specially formulated emulsion. All images courtesy of AMI
Key Contributors
The success of this ambitious project was made possible through collaboration. After the prime contractor, Milestone, crushed and sized the RAP stockpile, AMI, HRG and Pavement Maintenance Systems (PMS) managed the creation of the CCPR mixture at the central processing yard. PMS’s John Seabrooks operated the mobile mixing plant, while Wehr and Tim Zahrn of AMI supported the process, with HRG engineer Zach Robinson, who designed and tested the product mix.
Financial Impact
CCPR offers an alternative to conventional construction methods. For State Route 236, CCPR worked in place of an additional stone base and intermediate HMA layers. By using 100% of existing materials and reducing transportation costs, CCPR was 30% more cost-effective for the state than its HMA counterpart. The combination of FDR and CCPR also allowed for treatments at greater depth but at a lower cost per square yard, resulting in cost-effective, long-term pavement performance.
“If designed appropriately and used in the correct application, CCPR has comparable durability to traditional treatments,” explains Zach Robinson, Senior Engineer of Pavement Research at HRG.
Sustainability and Long-Term Environmental Impact
On top of cost-efficiency, CCPR reduces greenhouse gas emissions by up to 50% compared to conventional construction methods, positioning the technology at the intersection of smart economic decisions and greener solutions. In recent years, the federal government has begun incentivizing carbon-conscious materials and offering grants to support the reduction of greenhouse gases.
INDOT has secured several grants that underscore the state’s commitment to environmentally conscious practices. The Federal Highway Administration’s “Climate Challenge” grant will help benchmark the environmental impact of pavement materials. Meanwhile, the funding awarded to INDOT from the Low-Carbon Transportation Materials (LCTM) grants program will support the adoption of materials and products with lower embodied carbon. By expanding its cold recycling initiatives and actively capturing federal funding, INDOT is steadily advancing its sustainability goals.
Indiana is one of many states committed to adopting more sustainable practices, including improving energy efficiency and reducing reliance on traditional material resources. Cold recycling treatments like CCPR support the components of a strategic and sustainable infrastructure plan, helping states improve their pavements while reducing lifecycle emissions.

The team paved two 3-inch lifts with the CCPR mix prior to a 2-inch surface layer of hot-mix asphalt.
Future Projects
CCPR is gaining traction across the Midwest. Beyond INDOT’s six projects, PMS and AMI have completed more than 10 CCPR projects in Ohio, Michigan and Illinois. In addition to states in the Midwest gaining traction with these processes, the Virginia Department of Transportation (VDOT) continues to lead with their adoption of cold recycling into highway reconstruction projects like I-81 and I-64. Their work further demonstrates the successful use of cold recycling technology on higher-volume interstates.
The SR 236 project showcases how innovative techniques like CCPR can redefine modern road construction. By combining cost efficiency, sustainability and adaptability, CCPR not only strengthens infrastructure but also reduces environmental impact.
As more agencies recognize the long-term benefits of cold recycling, its adoption is likely to grow — paving the way for greener, more resilient roadways across the nation. With key players like INDOT, AMI and HRG leading the charge, the future of sustainable infrastructure is promising.