Pilot Project Brings HIR to Northwest Wisconsin
BY Tom Kuennen
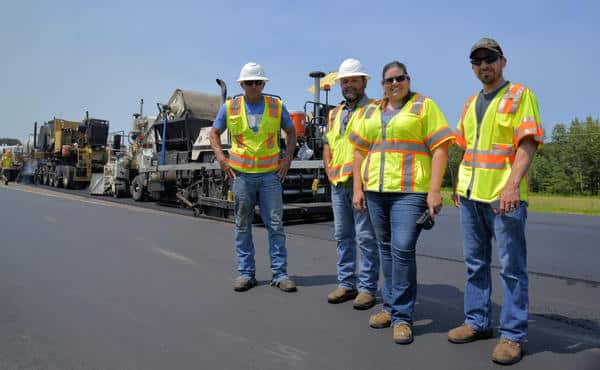
Wisconsin DOT and Dustrol use HIR to restore S.R. 64 in Dunn County
Last summer, a hot in-place recycling (HIR) pilot project brought the 100% recycle process to the Wisconsin DOT (WisDOT) Northwest Region.
“I was part of a team that helped bring this project to Wisconsin,” said WisDOT Northwest Region Pavement Engineer Devin Harings, P.E. “We’re trying out the HIR process. It’s one of the first times seeing it, and we’re still learning. Working with the contractor, we are seeing if we have to change the specification or if we like it as-is. To me, it’s a new treatment and specification and we’re looking to make adjustments as needed.”
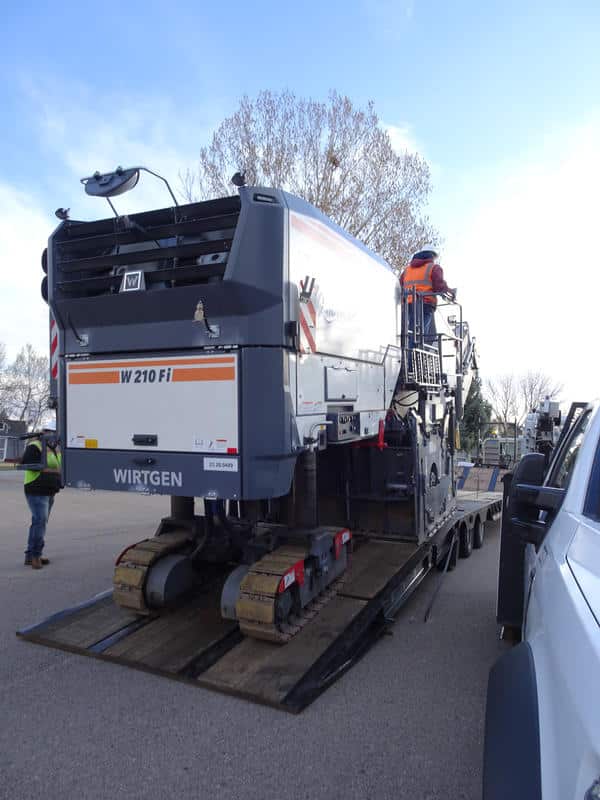
HIR, according to FP2 Inc., is a continuous process with a self-contained train of equipment that heats the distressed surface to 250 to 300°F, mills or scarifies a depth of ¾ to 2 inches, mixes it with new, rejuvenating asphalt emulsion or binder, places the recycled mix with a paver, and compacts the mat in readiness for potential new, or no, surfacing as dictated by the traffic and road conditions.
While scarification HIR had taken place in Wisconsin, there was only one other instance of HIR involving milling heads as part of the recycling train there, executed in 2024.
“As far as the process goes, we really like it,” Harings said. “Working with the contractor was great; their quality control and attention to detail really stood out…From start to finish, we were impressed and the outcome was better than what we expected.”
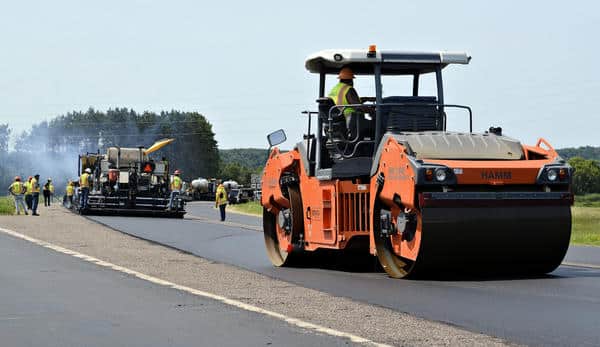
The rolling train included a Hamm HD+ 140i HV roller, using vibratory compaction, and a Hamm HD+ 140 VO finish roller in oscillation mode.
HIR should be only used on structurally sound pavements with good drainage, but with distressed surfaces, FP2 states. HIR has been successfully done on all types of roads, from city streets to rural roads to interstate highways. Before performing HIR, the reasons for the distresses should be analyzed so they can be corrected by the HIR process. Usually, an investigation by civil engineers will specify a process or mix design based on cores. The process has been detailed in AsphaltPro before.
Jessica Doud, project manager, WisDOT Northwest Region, spoke of the benefits of the process to the county.
“It’s a big thing,” Doud said. “We have a lot of miles up here, but not a lot of money to get everything done. So, if we can find something in-place that works, it helps.”
HIR is good for the environment, proponents say, because it uses 100 percent aggregates that already have been sourced, purchased, permitted, shot, hauled, crushed and screened, and shipped to a job site. Also, eliminating haul traffic is good for rural roads, and good for reducing air pollution including fugitive dust. “I think the DOT staff in Madison is aware of the benefits,” Doud added.
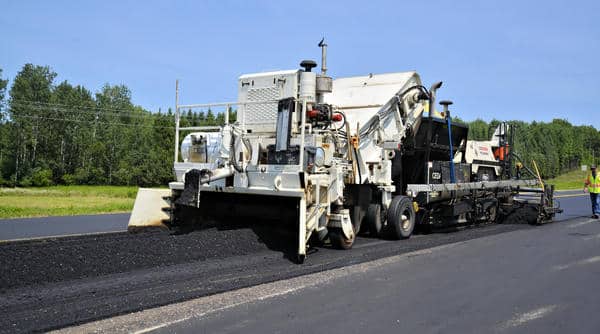
The windrow elevator lifts the recycled material and feeds it to the paver, which places a 2-inch lift.
S.R. 64 in Dunn County
The S.R. 64 project in Dunn County was 12.46 lane miles, or 233,432 square yards in size, and was undertaken by Dustrol Inc.,Towanda, Kansas. Some 26,000 tons of existing asphalt pavement was recycled on S.R. 64. (Dustrol also constructed the 2024 HIR project.)
The 2-inch recycled layer was to be overlaid with a chip seal. The recycle mix design and rejuvenator spec were developed from over 60 cores of the existing pavement that were taken and analyzed by Colas in Tulsa. Currently, S.R. 64 handles 1,500 to 4,000 vehicles per day, Harings added.
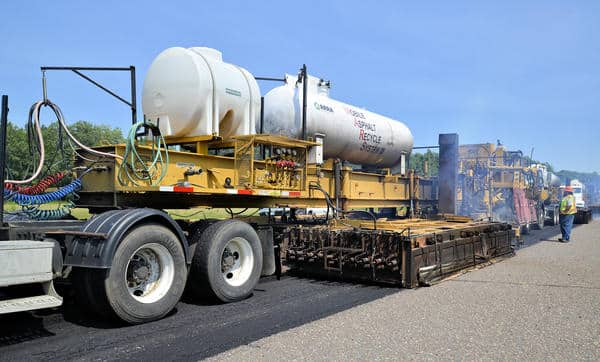
Dustrol’s Mobile Asphalt Recycling System, or MARS®, constitutes its newest method of rejuvenating asphalt pavements up to 2 inches or more. Here we see the third heater in the HIR train applying gentle heat into the existing material.
An ARA2P 3% polymer-modified emulsion was used to rejuvenate the heated asphalt pavement during the process, added at a rate of under 0.35 gallons per square yard recycled per plan. A total of 78,199 gallons of emulsion were to be used, supplied by Flint Hills Resources in Stevens Point, Wisconsin.
“The road was in rough shape,” Harings said. “The environmental aspects of recycling and sustainability are great, but we definitely need a lower-cost treatment because we have so many roads in poor shape, and there’s only so much money to go around.”
Harings estimated that the pavement condition index (PCI) of the highway was in the 30s. “That’s typically when we will treat a lot of our roads,” he said. “We’d like to do it a lot sooner, but just doesn’t happen.”
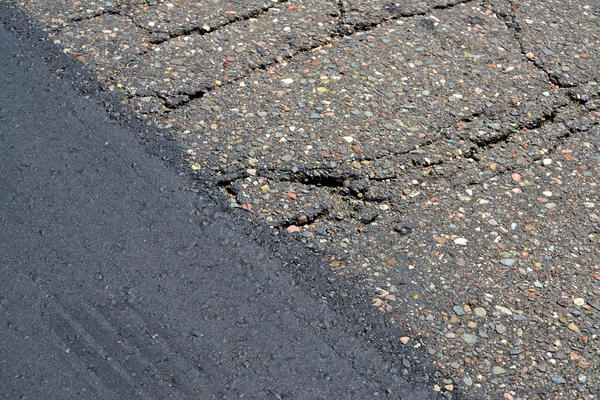
Here you can see the old pavement of State Route 64 in Dunn County and the new surface after the hot in-place recycling (HIR) treatment.
Multi-unit Process
Dustrol’s Mobile Asphalt Recycling System, or MARS®, constitutes its newest method of rejuvenating asphalt pavements up to 2 inches or more.
This HIR process typically uses eight units, one after the other, slowly moving forward and gently heating the existing asphalt pavement to the optimum level without prematurely aging or oxidizing the material.
The process begins with two or more custom-made, propane-fueled preheaters. The next heater in the train is equipped with grade-controlled milling drums, which windrow the top 1 inch of material. The milling heads are capable of milling 15 feet wide and 1 inch deep.
Tunnel heaters heat the underlying pavement while maintaining the temperature of the windrow. The surface is then milled and heated by up to three more milling heaters followed by tunnel heaters, depending on material and depth.
The last milling heater in the process has a metering system that injects and mixes a rejuvenating agent or asphalt emulsion into the milled asphalt and aggregate. No pug mill is used.
After adding and mixing the rejuvenating agent, the windrow is picked up with a conventional elevator. The paving process is performed with a conventional electronic grade control, electric screed paver. The material is compacted using conventional rollers in vibratory and static modes. The road can be opened to traffic after a cool-off period similar to an HMA paving operation, typically within an hour after the process is complete.
“Four units are preheaters, and four are heater/mills, and they’re alternated in the train,” said Donn Johnson, Sales and Marketing consultant for Dustrol. “The first preheater unit heats the aged asphalt down to a half inch and leaves it in place,” Johnson said. “The next heater comes and heats that same surface, but at the back it has milling heads, and it mills the material again to about a half inch. At the end it has guardrails that create a windrow in the center of the pavement.”
Heating the recycled material in stages precludes premature oxidation, providing relatively gentle heat, in one stage after the other, instead of an intense, single burst of heat. The paver places the resulting mix at a depth of 2 inches.
On this job, a Hamm HD+ 140i HV roller used vibratory compaction in the breakdown position, and a Hamm HD+ 140 VO finish roller in oscillation mode followed. The contractor generally can recycle between two and three lane miles per day.
Edited by AsphaltPro staff from editorial material provided by Dustrol Inc. (www.dustrol.com). Tom Kuennen is a freelance writer in the construction industry, (www.expresswaysonline.com)